Why Automation Still Depends on Shop-Floor Discipline
A secondary wood products manufacturer usually knows where automation will be difficult before a robot, scanner, or nested-based machining cell arrives. The trouble is visible in late job releases, undocumented fixture changes, exception handling, finishing delays, installation-driven revisions, maintenance response, and production knowledge carried by a few experienced employees.
A new cell makes those habits harder to ignore.
Modernization Meets Shop Reality
Canadian cabinet, millwork, furniture, store fixture, and architectural woodwork manufacturers are under pressure to modernize. Many have steady demand, tight labour markets, and customers asking for shorter lead times on increasingly customized work. Robots, sensors, simulation software, machine vision, CNC optimization, and machine learning all have a role to play. The harder work is fitting those tools into plants built around local knowledge, manual adjustment, material variation, and long-standing routines.
In “How Smaller Manufacturers Can Upgrade Their Tech,” Willy C. Shih and Ali Shakouri argue that post-pandemic supply-chain regionalization has created new openings for domestic small and medium-sized manufacturers. For Canadian secondary wood producers, that opportunity is tied less to commodity volume than to custom work: kitchens, institutional casework, fixtures, furniture components, and architectural interiors that depend on measurement accuracy, finish quality, and reliable delivery. Many firms survived earlier outsourcing cycles, but slow growth left them with older equipment and limited reason to invest in newer digital tools.
Where Automation Exposes Weakness
The first constraint is often confidence. Shih and Shakouri note that smaller manufacturers hesitate to change processes that have worked for years, particularly when customers continue to press on cost and new technologies require unfamiliar skills. A cabinet cell may depend on manual checks that an experienced operator can perform quickly. A finishing area may rely on one person’s judgment about drying, sheen, or colour matching. A supervisor may manage scheduling with a spreadsheet because the formal system cannot reflect late site measurements, revised drawings, hardware substitutions, or missing material.
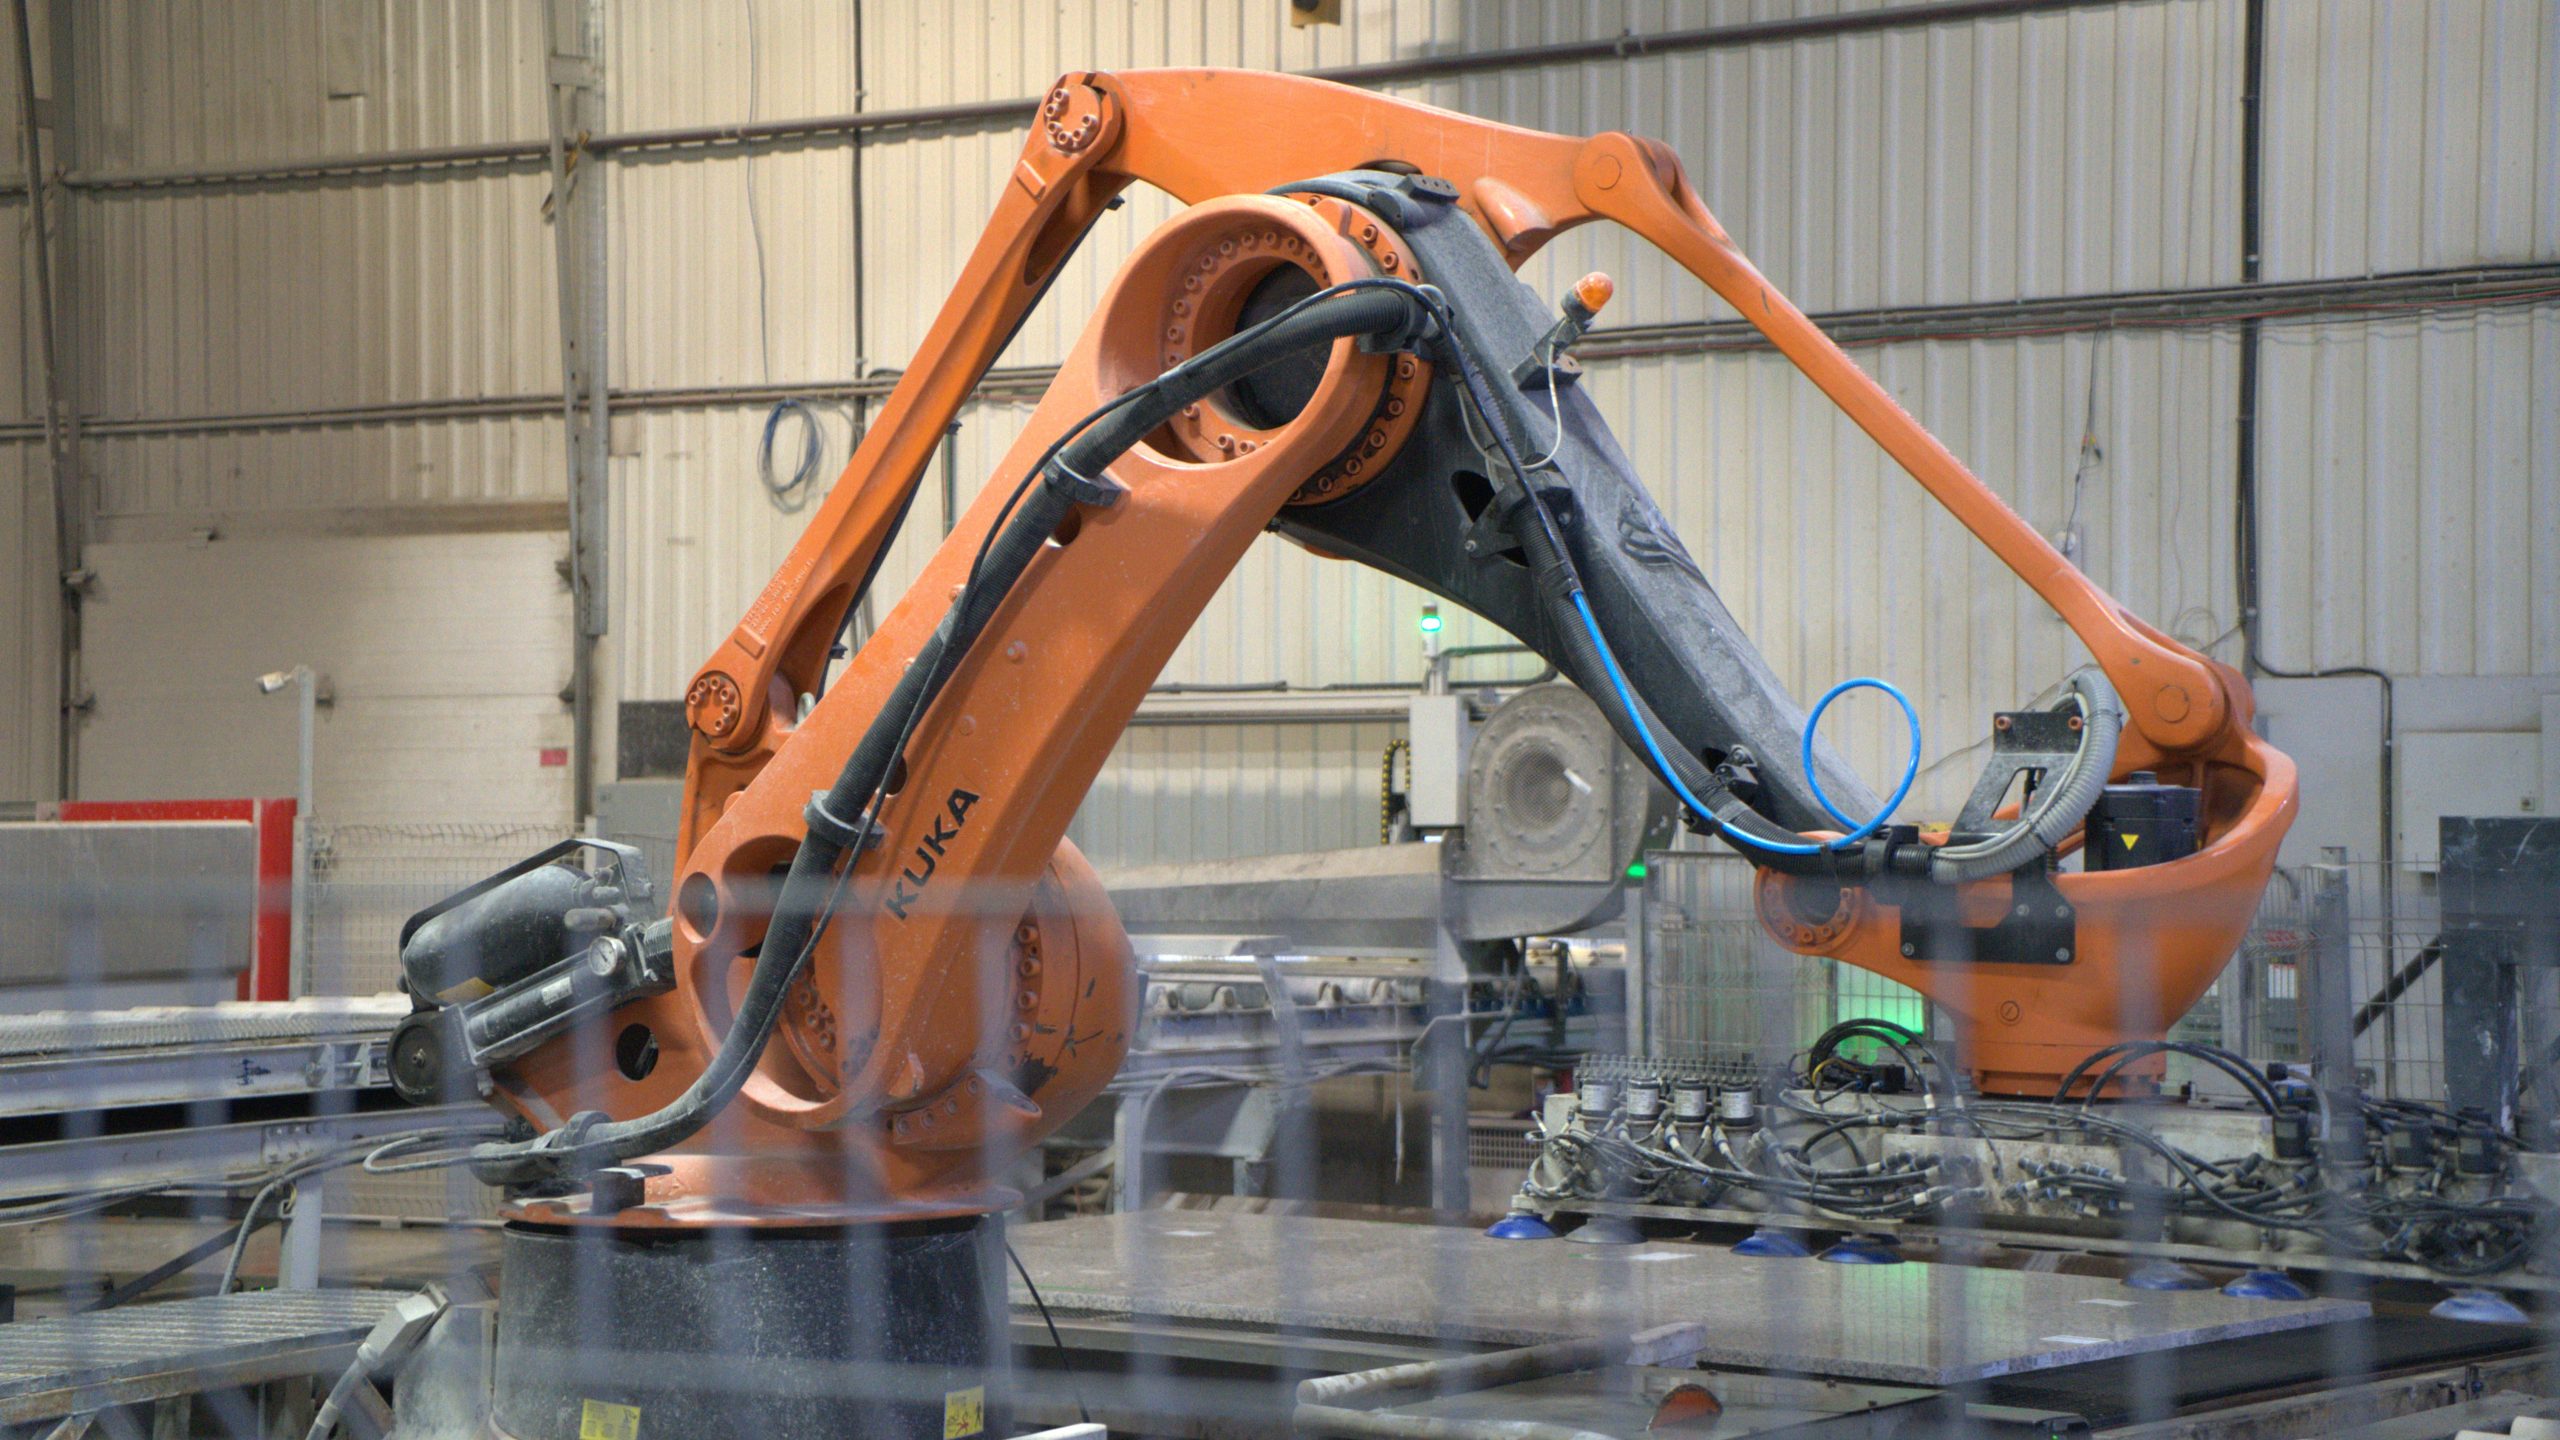
Automation puts pressure on those local fixes. A robot loading panels or parts needs predictable presentation, stable programs, clear recovery procedures, and someone who understands what to do when the cell stops. A machine-vision system needs consistent lighting, clean data, and agreement on what counts as a defect. A digital twin or production simulation needs enough process discipline for the model to describe actual work. In wood manufacturing, that also means accounting for grain, sheet yield, veneer handling, edge quality, finishing constraints, and the sequence between shop production and installation.
Steffen Fuchs, Ani Kelkar, and Ben Armstrong make a related point in “How to Successfully Automate in Manufacturing.” They describe Rimeco, an Ohio manufacturer that had strong demand after the pandemic but not enough workers. The company deployed a robot to load and unload machine parts. Employees did not adopt the system, the robot got stuck, and the company realized it lacked the programming and process-modification capabilities needed to make the installation useful. Rimeco later revisited automation with stronger leadership attention and a more deliberate operating plan.
Start With the Work
The pattern is familiar in wood shops. A pilot works in a narrow test, then struggles when exposed to production variability. Executives may expect labour savings. Engineers or programmers may focus on technical performance. Operators may worry that the new system will make their jobs harder or less secure. Finance may measure payback too narrowly. Maintenance may inherit equipment it did not help specify. The project can be technically plausible and still lack a stable owner.
Successful automation efforts usually begin with the work itself. What does the job require from operators? Where does variation enter the process? Which stoppages are predictable? Which decisions happen outside the formal system? In a cabinet or millwork plant, those questions often lead back to estimating, engineering, cutlisting, finishing, hardware staging, and installation coordination. They are less dramatic than a capital purchase, but they usually determine whether the equipment will run.
Measure Before Moving Equipment
In some plants, the answer points to simulation before equipment. Shih and Shakouri cite Pelco Products, an Oklahoma manufacturer of traffic and utility products, which used digital simulation to test production-flow changes before moving equipment. The model helped the company see bottlenecks, evaluate scenarios, and avoid rearranging the shop based only on opinion or habit. The same logic applies to a wood shop deciding whether congestion is caused by machining capacity, sanding, finishing, assembly, or late engineering releases.
Other plants may need better operating data first. TMF Center installed inexpensive power-consumption sensors to understand usage patterns and develop real-time dashboards. Kirby Risk Manufacturing experimented with sound sensors and machine learning to detect quality issues during operations. Primient used imaging to bring more precision to evaluating sugar-crystal size distribution. In a secondary wood plant, comparable projects might begin with CNC utilization, edgebander downtime, finishing rework, sanding bottlenecks, or the number of jobs waiting for missing hardware. Each turns a production signal into information managers and operators can use.
Manufacturers should begin where uncertainty is already costing time, capacity, or quality. A sensor that shows when a CNC router is idling may be more useful than a robot installed into an unstable process. A dashboard that shows bottlenecks between cutting, banding, drilling, sanding, finishing, and assembly may produce more immediate value than a complex AI project.
Bring the Workforce In Early
The workforce piece has to be handled early. Shih and Shakouri describe Rise Manufacturing, where employees were wary of a collaborative robot because they thought it might replace them. The Oklahoma Manufacturing Alliance helped the company trial the equipment, and workers saw that the robot could reduce variability in a manual polishing process while moving people into better jobs. In wood manufacturing, the same issue shows up when automation changes sanding, loading, inspection, material handling, or repetitive assembly work.
Budget for Integration
Larger manufacturers face the same problem at scale. Fuchs, Kelkar, and Armstrong argue that many automation failures come from integration breakdowns involving equipment, IT systems, workflows, and internal capabilities. They also note that hardware may represent only a minority of total system cost, with much of the expense tied to configuration and integration. Wood manufacturers used to buying machines as discrete assets have to budget and manage automation differently.
Leadership structure becomes important once automation affects quality, throughput, staffing, maintenance capacity, customer commitments, and data architecture. Fuchs, Kelkar, and Armstrong point to companies that have elevated automation through roles such as chief automation officer or cross-functional governance structures. In a smaller Canadian wood shop, the equivalent may be less formal: a production manager, programmer, estimator, and installer meeting regularly to decide which process problems are ready for automation and which still need basic control.
Build Capability, Not Just Capacity
For smaller manufacturers, the practical path is usually incremental and structured. Shih and Shakouri emphasize the role of manufacturing extension partnerships, university programs, state grants, and peer networks in helping companies test digital tools and reduce early adoption risk. Canadian secondary wood manufacturers can apply the same principle through industry associations, machinery suppliers, software vendors, colleges, and peer shops willing to share what worked and what did not. Outside support is most useful when it helps the company build internal capability.
Automation is commonly presented as a technology upgrade. On the floor, it tests how well the company understands its own work. The robot matters. So do the programs, fixtures, sensors, dashboards, maintenance routines, training plans, finishing schedules, hardware staging, and exception procedures around it.
Bibliography
Fuchs, Steffen, Ani Kelkar, and Ben Armstrong. “How to Successfully Automate in Manufacturing.” Harvard Business Review, September 22, 2025.
Shih, Willy C., and Ali Shakouri. “How Smaller Manufacturers Can Upgrade Their Tech.” Harvard Business Review, September 21, 2023.
 Tyler Holt is the Editor of Wood Industry / Le monde du bois magazine. He has a master’s degree in literature and publication, and years of experience in the publishing and digital media industry. His main area of study is the effect of digital technologies on industrial and networked production.